


Introduction To Silicon Steel Coating Process (1)
Nov 27, 2023
Leave a message
GNEE Oriented Silicon Steel
Compared with hot-rolled silicon steel sheets, cold-rolled silicon steel sheets have the obvious feature of being coated with a layer of coating on the surface during the production process. This coating not only has high insulation properties, but also has corrosion resistance and processability. , good heat resistance, the surface coating of oriented steel can improve the magnetic properties. The interlayer insulation of the finished hot-rolled silicon steel sheet is mainly completed by soaking in varnish and pickling and then drying. Let me introduce to you the coating process of silicon steel:
The insulating coating currently used for non-oriented silicon steel is an inorganic-organic hybrid insulating coating, referred to as a semi-organic coating (T4 chromate-organic resin): T0: water, boric acid (H3BO3), chromic anhydride (CrO3), Additives, etc.; T0 specific gravity (1.161~1.175g/cm3, 25°C).
The main reasons affecting the quality of coating fluid
(1) Effect of temperature
As the temperature increases, the effective storage time of T4 coating liquid shortens, namely 10°C-5 days, 20°C-3 days, and 30°C-2 days.
(2) Influence of time
At the same temperature, as time goes by, the color of the coating fluid becomes darker and darker, and finally deteriorates and is scrapped. Due to the influence of temperature on the coating liquid, the coating system has a separate refrigeration system, using water as the medium. The circulation pump passes cold water into each cooling point (including the circulation tank and the storage tank). There are snake-shaped tubes distributed in the tank, and the cold water Continuous circulation in the tube keeps the temperature of the coating fluid at <20°C. This ensures the freshness of the coating fluid.
Due to the influence of time on the coating liquid, the coating liquid should be used up as soon as possible during the production process, and then fresh coating liquid should be added to prevent the coating liquid from deteriorating and causing poor coating; when the unit encounters failure and maintenance, it should be Stop the installation system, promptly empty the coating fluid in the circulating tank and storage tank, and flush with water to prevent the coating fluid from clumping and clogging the pump and pipes after deterioration.
(3) Coating amount control
Coating amount: The weight of the coating per unit area of the steel strip, in g/m2. In order to ensure the comprehensive performance of the coating, various coatings must be tested in advance to determine the target value and control range of the optimal coating amount.
Factors affecting coating amount
(1) The specific gravity of the coating liquid: the higher the specific gravity, the higher the coating amount;
(2) Unit speed: Since the coating roller is a following roller, the coating amount is proportional to the unit speed. The higher the speed, the thicker the coating amount;
(3) Reduction of coating roller: The coating amount is inversely proportional to the reduction of coating roller. The greater the reduction, the thinner the coating;
(4) Roller shape of coating roller: The coating roller is made of acid-resistant rubber. Roller shape factors include the hardness, diameter, angle, depth, number of teeth, etc. of the rubber roller. The larger and deeper the groove, the more teeth, and the thicker the coating.
Equipment principle of coating roller
(1) Try to choose the same model of coating roller because of the roller type factor;
(2) Due to the effect of gravity, the coating amount on the lower surface is relatively thin, so a coating roller with high hardness, small diameter, and deep grooves should be used as the lower roller;
(3) Coating rollers must be replaced in pairs.
Adjust the spray angle and spray amount of coating fluid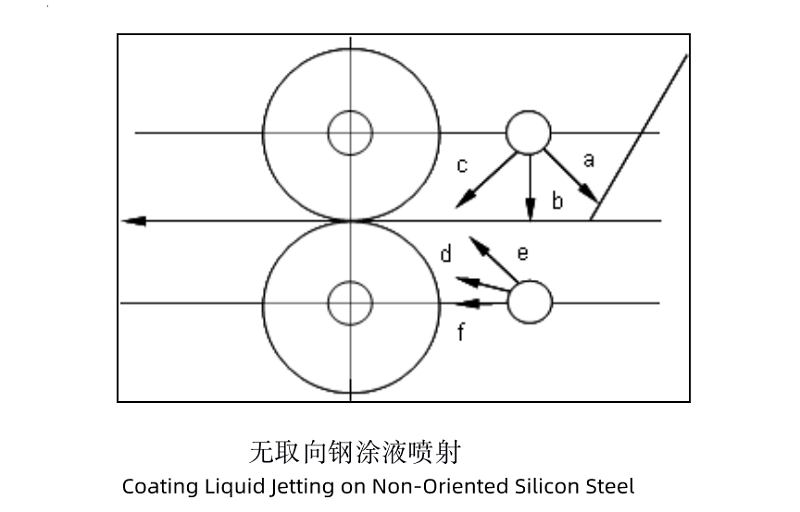
Among them, the injection directions of c and e are correct, other directions will cause coating defects.
The principle of adjusting the spray angle and spray volume of the coating liquid should ensure that the coating liquid is sprayed smoothly and evenly onto the coating roller without interruption, and prevent the spray pressure of the coating liquid from being too high or the spray direction of the coating liquid header. Was sprayed incorrectly. To generate bubbles, it is also necessary to prevent the spraying pressure of the coating liquid from being too low or the spraying direction of the coating liquid header being incorrect, resulting in no spraying of the coating liquid or spraying on the coating roller, resulting in coating defects such as missing coatings and spots.
Causes and Countermeasures of Main Defects in Coatings
(1) Missing coating:
Reason: It is caused by clogging of nozzles, headers, circulation pumps and other equipment, incorrect spray angle pressure of the coating fluid or insufficient coating fluid.
Countermeasures: Check frequently during operation, clear and clean the header in time, and adjust the injection pressure and angle of the header.
(2) Double line:
Reasons: The specific gravity of the coating liquid is too high; the viscosity of the coating liquid is high; the hardness of the coating roller is high; the reduction of the coating roller is small.
Countermeasures: Strictly standardize the liquid preparation operation, and control the proportion of the coating liquid within the target range according to the process; reasonably control the temperature of the coating liquid. High-temperature coating liquids are prone to aging, but if the temperature is too low, the viscosity of the coating liquid will be high and it will spread during coating. Slowly, double lines are produced (the optimal temperature is 10-20°C); the coating roller has high hardness, and double lines are easily produced during coating. Therefore, a coating roller with a lower hardness should be selected according to the speed of the unit, and the coating roller should be selected according to the actual coating situation. Reasonably adjust the dent amount of the coating roller.
(3) Uneven tone:
Causes: poor alkali cleaning, oil stains on the steel plate; uneven coating; aging of the coating roller; improper drying and firing temperature control, etc.
Countermeasures: Improve the quality of alkali cleaning; strictly control the coating amount according to the coating standards, and adjust the reduction of the coating roller in a timely manner to ensure that the coating amount on the entire steel plate surface is controlled within the target range, with the deviation as small as possible, thereby ensuring the coating . Uniform; if the coating roller is found to be aging, the coating roller should be replaced in time, and the temperature of the drying and sintering furnace should be reasonably controlled in a timely manner according to changes in the unit speed.